Related Topics:
Explosion Proof Pipe Inspection-
Principle of Automatic Visual Inspection of Fiber Optic Patch Cords
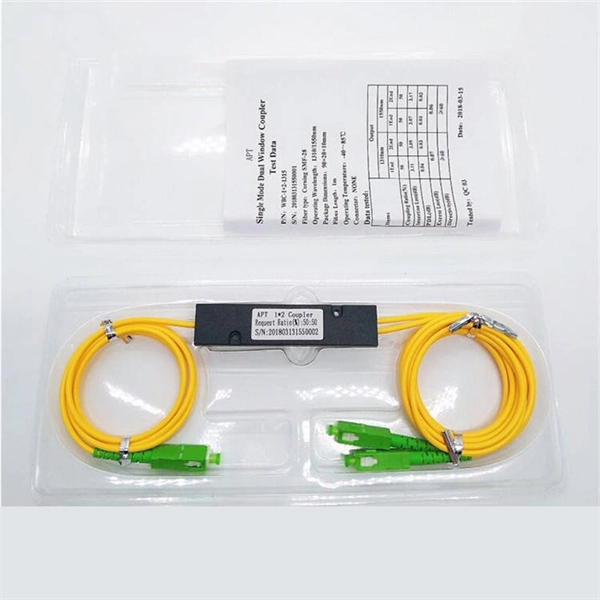
Endface inspection focuses on the visible quality of the polished fiber surface and surrounding ferrule area. You use a fiber microscope or automated inspection scope to check for contamination, pits, chips, cracks, and scratches. Even a small dust particle or scratch on the endface can increase insertion loss, reduce return loss, and introduce random link instability. The primary reason for fiber inspection is to ensure that the connectors are free of any defects, damage, or debris that would prevent sufficient transmission of light when mated. Normal Inspection Items for Fiber Optic Patch Cords Fiber optic patch cords are critical components in communication systems, connecting various devices and ensuring efficient data transmission. To maintain high-quality performance, a thorough inspection process is essential. The. FOCIS WiFi2 is an ergonomic Fiber Optic Connector Inspection System that, when paired with an iOS or Android smart device, provides fast and accurate IEC/IPC/AT&T compliant and user-defined pass/fail end-face cleanliness analysis. FOCIS Duel is a self-contained twin-ported Bluetooth connected fiber.
[PDF Version]
-
Fiber Optic Cable Sheath Inspection Section
The procedures in this document describe basic inspection techniques and processes of cleaning for fiber optic cables, bulkheads, and adapters used in fiber optic connections. These types are (Figure 1): Type A 1) The sheath is peeled or chipped. 2) No portion of the armor or cable core is exposed. After cable placement is complete the residual tension on the cable should be less than this value. NOTE: Steps that reference. There are three main principles that needs to be taken in consideration for an efficient optical connection: a perfect core alignment, perfect physical contact and dirt-free connectors.
[PDF Version]
-
On-site distribution box circuit inspection pricing
The cost of a distribution board inspection varies depending on the number of circuits, the complexity of the installation, and any additional measurements such as thermographic testing. Average prices range from €90 to €150 for a standard inspection, excluding any repairs or. We check everything down to the last detail: from distribution boards, fuse boxes, wiring, busbar distribution, and earth rods to connection terminals and smart circuits. You prevent power outages, significant repair costs, and potential fire risks in your home or business. This way, we guarantee. Expect to pay around £100–£300 for a domestic EICR in 2025, while commercial properties are usually priced £10–£20 per circuit. An EICR cost mainly covers the electrician's time and expertise.
[PDF Version]
-
Sample Inspection Report for Metal Distribution Boxes
This is a sample inspection report template. For every product inspection service, our technical team meticulously prepares a detailed inspection checklist, tailored to your specifications and the general inspection standard ANSI/ASQC Z1. It does not relieve the manufacturers from their contractual obligations nor prejudice client's right for compensation for any apparent and/or hidden defects not detected during our b xes, not e ss er is listed hereAn Inspection Report Template is a standardized document used by inspectors across various industries to record findings from an inspection process. It outlines a comprehensive checklist of criteria, benchmarks, and observations necessary to assess conditions, compliance with regulations, or. A material receiving inspection report enables material controllers to document the inspection and verification of incoming construction materials. A well-documented material. Ensure your materials meet the highest standards with the Material Quality Inspection Report Template, offered by Template. R: Document Review = Review means Review document, which includes of material test.
[PDF Version]
-
Relay Protection Inspection Procedures
During visual inspection, the relay should be checked for any signs of damage, such as physical wear and tear, loose connections, or corrosion. These devices spend years in standby mode, waiting to isolate faults in milliseconds when called upon. Yet without structured, documented maintenance, organizations often discover relay. The testing and verification of relay protection devices can be divided into four groups: Type tests are needed to prove that a protection relay meets the claimed specification and follows all relevant standards. Since the basic function of a protection relay is to correctly function under abnormal. Protective circuit functional testing, including lockout relay testing, must take place immediately upon installation, every 2 years thereafter, and upon any change in wiring. Acceptance tests fall into two categories : (i) On new relays which are to be used for the first time. Applications: Overcurrent. THEY SHOULD BE GIVEN FIRST LINE MAINTENANCE ATTENTION. ” relay may only need to operate for 0.
[PDF Version]
-
Relay Protection Inspection and Maintenance
Relay maintenance generally consists of : Inspection and burnishing of contacts. Adjustments checking (iv) Breakers tripped by manual contact closing. Most frequently they are performed by simulating test. Protective circuit functional testing, including lockout relay testing, must take place immediately upon installation, every 2 years thereafter, and upon any change in wiring. Protective relays are your most powerful defense against long, costly outages and extensive. Servicing protective relays per manufacturer and NETA recommendations ensures they work properly to prevent injury or extensive damage to your plant during an electrical distribution abnormality. To properly test relays, understanding their classification by design and application is essential. This. In the rapidly evolving industrial landscape of Electrical Equipment Manufacturing, the role of an Electrical Maintenance Engineer is more critical than ever. This article delves deep into.
[PDF Version]
-
Does the cable tray need to be sent for inspection
Regular cable tray inspection is essential to ensure electrical systems function safely and efficiently. Cable trays support and organize cables, preventing tangling, damage, and overloading. The process described here takes a systematic approach to ensuring that cable tray installations meet safety, reliability, and project-specific needs while following to. Thus while maintenance, installation and inspection of cable trays, the following concerns should be given attention. Cable. Cable Tray Inspection – Key Technical and Structural Considerations When inspecting cable trays, several technical and structural aspects must be checked to ensure safety, efficiency, and compliance with specifications.
[PDF Version]
-
Explosion-proof distribution box gas pipe
The explosion-proof distribution box safely delivers power in hazardous zones (oil, gas, chemical plants) with rugged, spark-resistant casing—ATEX/IECEx, IP66 certified for reliable operation in explosive environments. Explosion-proof lights used in hazardous areas where combustible gases and dust exist, which can prevent arcs, sparks, and high temperatures that may occur inside the lamp from igniting combustible gases and dust in the surrounding environment, thus meeting explosion-proof requirements. This article outlines the essential principles for connecting explosion-proof distribution boxes with galvanized pipes, providing practical details and best. From its global facilities ABB manufactures a wide range of ATEX, IECEx, UL, CSA approved electrical products for hazardous area applications. These include cable glands and lighting ranges. The products are examined for their shock explosion resistance by means of a gas explosion, dust explosion or stress analysis.
[PDF Version]
-
Spacing of Fire Pipe Cable Tray Installation Brackets
Traditionally, it has been recommended to install brackets approximately every 1 to 1. 5 meters along the length of the cable tray. There are factors to consider when determining the appropriate bracket spacing for your installation. Cable ladder systems and cable tray systems shall be manufactured in accordance with BS EN 61537, channel support. Although BS 7671 touches on the subject of cable supports, it does not detail specifically what these support distances should be. 8 (Other Mechanical Stresses (AJ)) in that document provides requirements for cable support. Distances Shown are applicable to Vertical & Horizontal Applications within a Flexible Wall, AAC. Cable trays and pipes serve as the backbone of electrical and fluid transportation systems in both residential and industrial environments.
[PDF Version]